Overview
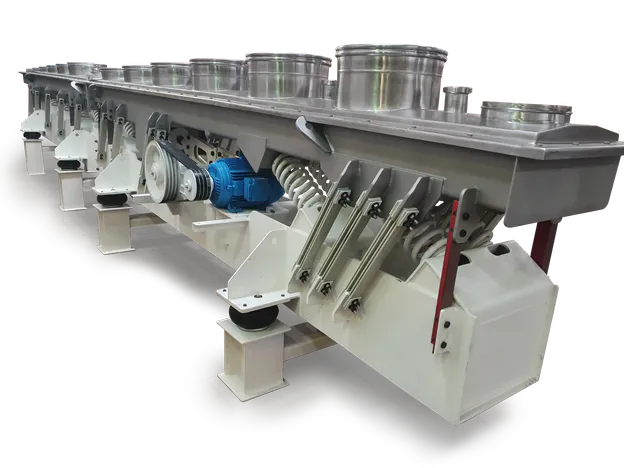
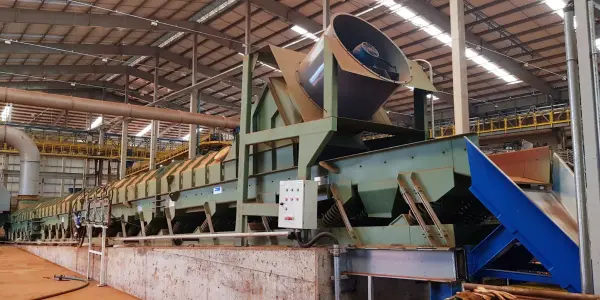
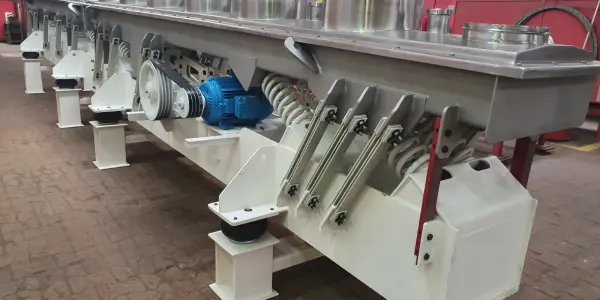
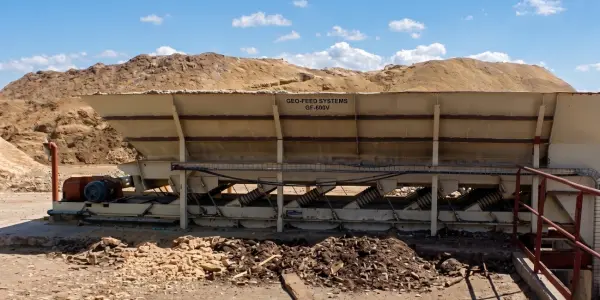
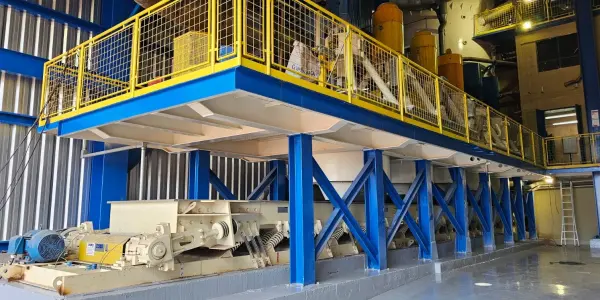
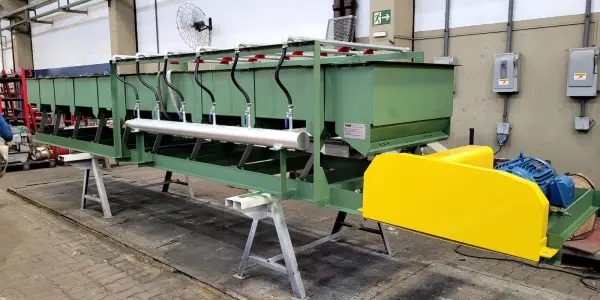
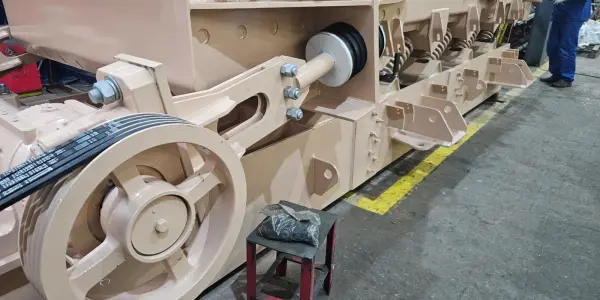
Since 1978, MAVI has provided solutions for transporting solids in demanding applications, focusing on low maintenance requirements and reduced operating costs. The REVITRAN® was developed drawing on the experience of UHDE’s former vibrating equipment division in Germany. Its performance relies on operating near the resonance range, leveraging this physical principle to achieve high energy efficiency and durability. Depending on the configuration, the equipment can achieve conveying lengths of up to 60 meters and handle high capacities. In addition to conveying, the REVITRAN® can be configured to cool parts, dry bulk materials, wash products, and perform screening while the material is being transported.
|
ATÉ 60 metros Comprimento de transporte, conforme aplicação |
FUNÇÕES INTEGRADAS Transportar, resfriar, secar, lavar e peneirar |
|---|